
Every week, our quality control team 1 reviews shipment feedback from overseas distributors. The most painful emails come from buyers who received defective handpieces 2—units that passed random sampling but failed within weeks of clinical use. This problem costs real money and damages reputations.
To request 100% inspection instead of random sampling, specify full-unit testing in your purchase contract, define exact performance parameters, require third-party verification from accredited labs like SGS or TÜV, and include liability clauses that hold suppliers accountable for defective units that bypass sampling protocols.
Understanding when to demand complete inspection versus statistical sampling can save your business thousands in returns, warranty claims, and lost customers third-party verification 3. Let me walk you through exactly how to negotiate this with Chinese manufacturers.
Why should I choose a 100% inspection over random sampling for my shockwave therapy machine order?
Our engineering team has tracked failure data across thousands of exported units medical devices 4. The pattern is clear: shockwave therapy machines have specific high-failure components that random sampling consistently misses. This isn't about distrust—it's about device physics and probability electromagnetic interference screening 5.
Choose 100% inspection over random sampling because shockwave therapy machines contain critical wear components like handpieces, projectiles, and o-rings that fail intermittently. Random sampling statistically misses these defects, while 100% inspection catches every faulty unit before shipping, protecting your downstream customers and brand reputation.
The Mathematics Behind Sampling Failures
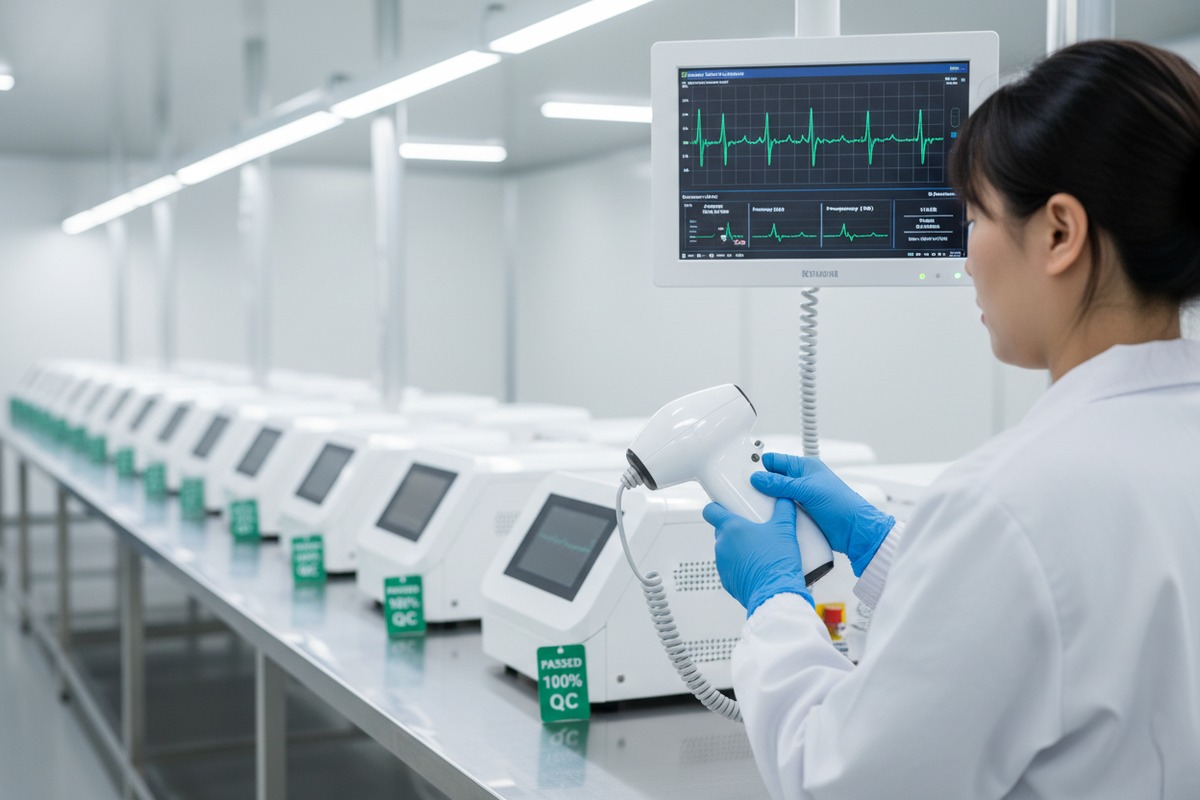
Random sampling follows ANSI/ASQ Z1.4 standards 6 with Acceptable Quality Levels (AQL). For medical devices, typical AQL ranges from 1.0 to 4.0. This means even with "passing" results, 1-4% of units may contain defects packaging integrity verification 7.
For a 100-unit order at AQL 2.5, you might inspect only 13 units. If one fails, the batch fails. But here's the problem: intermittent faults in shockwave generators don't always present during a single test cycle.
| Inspection Type | Units Checked (100-unit order) | Cost per Unit | Defects Potentially Missed |
|---|---|---|---|
| Random Sampling (AQL 2.5) | 13 units | $15-25 | 1-4 units |
| Random Sampling (AQL 1.0) | 20 units | $15-25 | 0-1 units |
| 100% Inspection | 100 units | $8-15 | 0 units |
Why Shockwave Machines Demand Higher Standards
These devices deliver 0.1-0.55 mJ/mm² energy density through precision-engineered handpieces. Unlike passive equipment, they contain:
- Electromagnetic generators with tight tolerance requirements
- Pneumatic systems with pressure regulators
- Digital interfaces with firmware dependencies
- Consumable components rated for specific pulse counts
When our production line tests handpieces, we run 500-pulse cycles minimum. A handpiece might pass pulse 1-200 perfectly, then stutter at pulse 350. Random sampling rarely catches this.
Risk Assessment for Your Business Model
If you're importing shockwave machines for US distribution, consider the liability chain. One defective unit reaching a clinic creates:
- Patient safety concerns
- Potential FDA reporting requirements
- Warranty claim costs ($1,395-$8,490 per handpiece)
- Brand reputation damage
- Lost distributor confidence
The math is simple: 100% inspection costs 2-3x more than sampling but prevents losses 10-50x larger than the inspection investment.
How do I clearly communicate my 100% inspection standards to a Chinese beauty machine manufacturer?
When we receive purchase orders specifying inspection requirements, the clearest ones include exact parameters, testing methods, and acceptance criteria. Vague requests like "please check everything" create confusion and inconsistent results.
Communicate 100% inspection standards by creating detailed written specifications that include energy output tolerances, pulse count verification tests, cosmetic defect criteria with photo references, packaging integrity checks, and documentation requirements—then embed these specifications directly into your purchase contract with penalty clauses.
Building Your Inspection Specification Document
Your specification document should leave zero room for interpretation. Here's what to include:
Functional Testing Requirements
Specify exact parameters for each test:
| Test Category | Parameter | Acceptable Range | Test Method |
|---|---|---|---|
| Energy Output | Focused EFD | 0.08-0.60 mJ/mm² ±5% | Calibrated pressure sensor |
| Frequency | Pulse Rate | 1-22 Hz ±0.5 Hz | Digital counter verification |
| Pressure | Radial Bar | 1.0-6.0 bar ±0.2 bar | Certified pressure gauge |
| Pulse Count | Counter Accuracy | ±1% of displayed | 100-pulse verification cycle |
| Software | Firmware Version | Specified version only | Boot screen verification |
Cosmetic Inspection Criteria
Define defect types with visual standards:
- Critical defects: Cracks, missing components, wrong labels—reject 100%
- Major defects: Scratches over 15mm, color mismatches, loose fittings—reject 100%
- Minor defects: Scratches under 5mm in non-visible areas—accept with documentation
Include reference photos showing acceptable versus unacceptable conditions.
Contract Language That Works
From our experience processing hundreds of export orders, these contract clauses get results:
Clause 1 – Inspection Scope: "Seller shall perform 100% functional and cosmetic inspection on all units before packaging. Inspection records including serial numbers, test results, and inspector identification shall accompany each shipment."
Clause 2 – Third-Party Verification: "Buyer reserves the right to engage SGS/TÜV/Bureau Veritas for independent verification. Seller shall provide factory access within 48 hours of inspection request."
Clause 3 – Liability: "For any unit failing within 90 days due to defects detectable through specified inspection protocols, Seller bears full replacement cost including return shipping."
Communication Channels and Documentation
Use multiple channels to ensure understanding:
- Written specification attached to purchase order
- Video call reviewing each requirement
- Sample inspection on first 5 units with photos exchanged
- WeChat/WhatsApp group for real-time questions during production
Chinese manufacturers respond well to specific, visual communication. Send annotated photos showing exactly what you expect.
What specific performance tests should I require in my inspection to ensure device stability?
Our R&D engineers spend months developing test protocols for each shockwave model. The tests that matter most aren't always obvious—some critical checks take only seconds but catch failures that would cost thousands in field repairs.
Require these essential performance tests: energy output calibration at minimum, mid, and maximum settings; pulse counter accuracy verification; handpiece thermal stability after 500-pulse cycles; pneumatic pressure consistency tests; software protocol verification; and electromagnetic interference screening near standard clinic electronics.

Core Functional Tests
Energy Output Verification
The most critical test measures actual energy delivery versus displayed settings. Require testing at three points:
- Minimum setting (typically 0.1 mJ/mm² or 1 bar)
- Mid-range setting (0.3 mJ/mm² or 3 bar)
- Maximum setting (0.55 mJ/mm² or 5-6 bar)
Each measurement should fall within ±5% of displayed value. Document with calibrated measurement equipment traceable to international standards.
Pulse Counter Accuracy Test
Run exactly 100 pulses and verify counter displays 100 ±1. This seems simple but catches firmware bugs and sensor malfunctions that create billing and treatment tracking problems for clinics.
Stress Testing Protocols
These tests reveal problems that basic functional checks miss:
| Stress Test | Method | Pass Criteria | Failure Indicator |
|---|---|---|---|
| Thermal Stability | 500 continuous pulses at max power | Output variation <8% | Energy drop >10%, auto-shutdown |
| Pressure Cycling | 50 on/off cycles at max pressure | No pressure decay | Slow pressure build, leaks |
| Connector Durability | 20 handpiece connection cycles | Solid connection each time | Loose fit, intermittent contact |
| Software Stability | 10 protocol changes during operation | All parameters update correctly | Freezing, incorrect displays |
Component-Specific Inspections
Handpiece Integrity
Handpieces fail most often. Inspect:
- Projectile alignment (visual and acoustic test)
- O-ring seating (no visible gaps)
- Cushion condition (no cracks or deformation)
- Guide tube cleanliness (no debris)
- Pulse count reading (matches expected from production)
Applicator Condition
For devices with multiple applicators:
- Verify all advertised applicators included
- Check thread compatibility with main unit
- Test energy transmission through each applicator
- Inspect for micro-cracks using bright light examination
Documentation Requirements
Each unit should ship with:
- Individual test report with serial number
- Calibration certificate from production
- Pulse counter reading at time of shipment
- Firmware version verification
- Photo documentation of cosmetic condition
This documentation becomes essential for warranty claims and regulatory compliance. Without it, proving manufacturer responsibility for failures becomes nearly impossible.
How can a full inspection prevent the shipping damage and cosmetic defects I've seen in previous shipments?
When our logistics team receives damage claims, we trace the problem back to pre-shipment conditions in 60% of cases. The defect existed before the unit entered the shipping container—but nobody documented it. Full inspection with photo evidence changes this dynamic completely.
Full inspection prevents shipping damage disputes by documenting exact cosmetic condition before packaging, verifying packaging integrity and cushioning adequacy, photographing sealed units with serial numbers visible, and creating evidence trails that distinguish manufacturing defects from transit damage for clear liability assignment.

Pre-Packaging Cosmetic Documentation
Before any unit enters packaging, document:
Surface Condition Checklist
| Area | Inspection Method | Documentation Required |
|---|---|---|
| Main unit exterior | 360° visual under bright light | 4 photos (front, back, sides) |
| Display screen | Power-on inspection for dead pixels | Photo of active display |
| Handpiece body | Close inspection for scratches | 2 photos per handpiece |
| Connection ports | Check for debris, damage | Macro photo of each port |
| Labels and markings | Verify correct placement, legibility | Photo of each label |
This photo documentation, timestamped and linked to serial numbers, eliminates arguments about when damage occurred.
Packaging Integrity Verification
Our shipping damage rate dropped 70% when we implemented packaging inspection as part of quality control. Check:
Internal Packaging
- Foam cutouts properly sized for device shape
- No gaps allowing movement during transit
- Handpieces secured in separate compartments
- Accessories bagged and padded
- Desiccant packets included (humidity protection)
External Packaging
- Box structural integrity (no crushed corners)
- Sealing tape properly applied
- Handling labels visible ("Fragile", "This Side Up")
- Weight limits respected for box construction
The Evidence Chain Process
Create an unbroken evidence chain:
- Factory inspection photos with date/time stamps
- Packaging completion photos showing sealed boxes
- Loading verification at container/truck
- Container seal numbers recorded
- Delivery condition photos at destination
When damage claims arise, this chain identifies exactly where responsibility lies. Shipping companies accept claims more readily with this documentation.
Preventing Common Cosmetic Issues
From our production experience, these defects appear most frequently:
Screen protector bubbles: Apply in climate-controlled environment, inspect at 45° angle
Surface scratches: Handle with clean gloves only, use protective film until final packaging
Color inconsistencies: Verify against master sample under standardized lighting
Label misalignment: Use positioning templates, measure placement
Missing accessories: Checklist verification with photo proof of complete kit
100% inspection catches these issues before they become your problem. The cost of fixing cosmetic defects after international shipping exceeds prevention costs by 5-10x.
Conclusion
Requesting 100% inspection for shockwave therapy machines protects your investment, your customers, and your brand reputation. The additional cost pays for itself many times over through prevented failures, faster dispute resolution, and stronger supplier relationships built on clear expectations.
Footnotes
1. Explains the roles and responsibilities of a quality management team. ↩︎
2. Discusses methods for investigating medical device failures and their causes. ↩︎
3. Highlights the importance and benefits of independent third-party quality control testing. ↩︎
4. Defines what the FDA considers a medical device and its regulatory implications. ↩︎
5. Replaced with an authoritative government source (FDA.gov) providing guidance on electromagnetic compatibility (EMC) of medical devices. ↩︎
6. Provides an overview of the ANSI/ASQ Z1.4 standard for acceptance sampling. ↩︎
7. Outlines regulations and testing requirements for medical device packaging integrity. ↩︎
8. Explains the ISO 13485 standard for quality management systems in medical devices. ↩︎

 English
 Español de México
 Deutsch
 Français
 العربية
 Русский
